 Aberdeen-headquartered well integrity and decommissioning specialist Unity has completed a technically challenging well intervention project in Central Italy for SMAPE, delivering a bespoke thru-tubing solution for a major international oil company.
The project required an alternative approach after conventional cement squeeze operations failed to achieve the necessary well isolation. Cement was being absorbed by a thief zone located behind a slotted liner, preventing the operation from delivering the required result.
The well’s geometry presented a further challenge. Standard mechanical isolation equipment could not be used because the retainer needed to pass through a tight 2.188-inch nipple restriction before expanding and setting securely within a 3.958-inch ID above the thief zone.
Planning also had to account for the well’s low fluid level. This was necessary to prevent premature disconnection during the cementing operation and ensure the treatment packer was not pressurised beyond its operating limitations.
Unity responded by engineering an inflatable cement retainer capable of passing through the restricted nipple profile. The solution was developed after attempts to achieve isolation using cement alone had proved unsuccessful.
Rather than relying on an off-the-shelf product, Unity selected components from across the OEM market and engineered them to suit the specific requirements of the well. This OEM-agnostic approach allows its thru-tubing team to develop tailored solutions for complex intervention challenges.
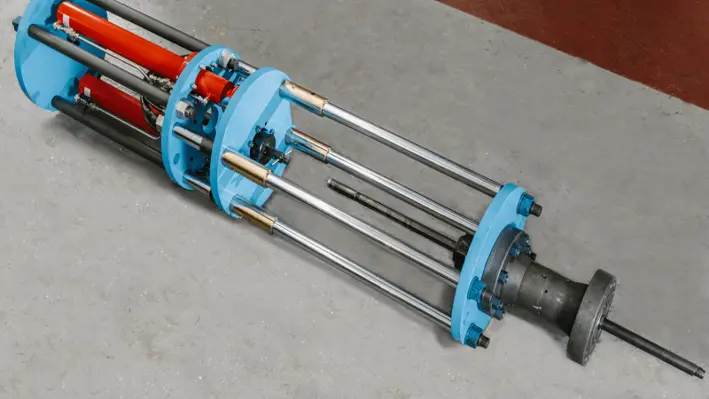
For the project, Unity’s specialist thru-tubing team developed a custom 2.125-inch inflatable cement retainer. The Bottom-Hole Assembly was modified with a dual check valve system and shear disconnect, while a cement plug was incorporated into the solution.
This configuration enabled the rig team to release from the cement retainer immediately after the squeeze operation without dropping additional balls or facing complications after the packer had been inflated.
Unity Thru-Tubing Operations Manager Chris Myles said: “This is the first time we have used this configuration, which draws on established principles. This is really the heart of how we work at Unity thru-tubing. We're not tied to one OEM's solution, so we can pull in whatever's most appropriate, adapt it, and build something that fits the exact problem in front of us. That's what sets Unity apart, and it's what clients get in return - a solution built around their well requirements, not the other way round.
“This project marks our second collaboration with SMAPE, and it’s fantastic that the team see the value we bring to complex well integrity challenges. These are often the kinds of jobs where a standard approach isn’t enough, so being able to work closely with the client and develop a solution around the specific requirements of the well is where our expertise really makes a difference.”
The project forms part of Unity’s wider investment in well intervention capabilities. Since the beginning of 2025, the company has expanded its intervention tooling portfolio, strengthening its ability to deliver integrated well integrity and intervention services through a single supplier relationship.
By combining engineering expertise, OEM-agnostic tool selection and operational experience, Unity provides operators and service providers with customised solutions for complex well integrity requirements. The approach is also designed to streamline operations by reducing the cost and complexity associated with managing multiple suppliers.
Unity is part of the FrontRow Energy Technology Group and has a 30-year track record of supporting operators worldwide in reducing risk, overcoming operational constraints and extending asset life across energy operations.
SMAPE is an independent engineering company specialising in coiled tubing and well services.